
What's Happening?
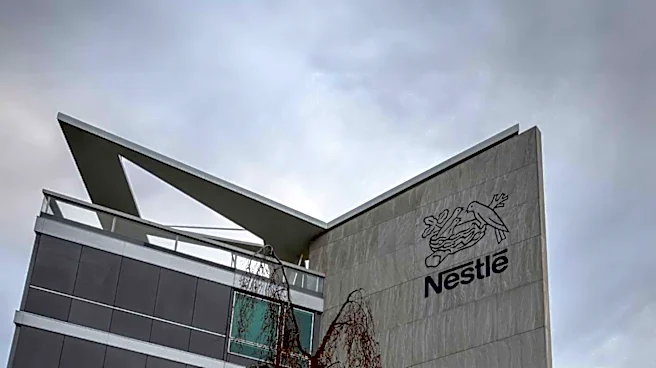
Nestlé, the world's largest food and beverage company, is actively seeking a Manufacturing Excellence Specialist for its Chembong Factory in Negeri Sembilna. This role is crucial for driving continuous improvement processes, implementing factory initiatives,
and ensuring sustainable performance enhancements. The specialist will focus on cost reduction and maintaining the competitiveness of Total Delivered Cost while upholding Nestlé's quality standards. Key responsibilities include leading and facilitating process improvement initiatives, conducting focused improvement projects, and implementing continuous improvement tools such as Six Sigma, Lean Manufacturing, and 5S. The position requires a degree in Chemical Engineering or a related discipline and 3-5 years of relevant experience, with proficiency in data analysis and a background in manufacturing, preferably in FMCG.
Why It's Important?
The recruitment of a Manufacturing Excellence Specialist by Nestlé underscores the company's commitment to operational efficiency and cost optimization, which has significant implications for the U.S. food and beverage industry. As a global leader, Nestlé's adoption of advanced manufacturing practices and continuous improvement methodologies can set benchmarks for other companies operating in the U.S. This focus on efficiency and cost reduction can lead to more competitive pricing for consumers and potentially influence supply chain management strategies across the industry. Furthermore, the emphasis on maintaining quality standards while reducing costs highlights a critical balance that U.S. manufacturers also strive to achieve, impacting product safety, consumer trust, and regulatory compliance. The skills sought, such as Six Sigma and Lean Manufacturing, are highly valued in the U.S. manufacturing sector, indicating a broader industry trend towards data-driven operational excellence.
What's Next?
The successful integration of a Manufacturing Excellence Specialist at Nestlé's Chembong Factory is expected to lead to tangible improvements in production efficiency and cost savings. These localized improvements, if successful, could be scaled and replicated across Nestlé's global network, potentially influencing manufacturing practices in its U.S. facilities. The continuous improvement initiatives, including the implementation of tools like Six Sigma and Lean Manufacturing, will likely result in optimized production processes, reduced waste, and enhanced product quality. This could translate into more consistent product availability and potentially more competitive pricing for U.S. consumers. Furthermore, Nestlé's ongoing investment in operational excellence may encourage other U.S. food and beverage companies to adopt similar strategies to remain competitive in a dynamic market.
Beyond the Headlines
Beyond the immediate operational benefits, Nestlé's pursuit of manufacturing excellence reflects a broader industry trend towards leveraging data and advanced methodologies to achieve sustainable growth. The emphasis on continuous learning and the ability to challenge and improve business processes suggests a corporate culture that values innovation and adaptability. This approach can have a ripple effect, fostering a more skilled workforce and promoting best practices in manufacturing across the U.S. food and beverage sector. The role also highlights the increasing importance of technical expertise, such as chemical engineering and data analysis, in modern manufacturing environments. This could influence educational and training programs aimed at preparing the next generation of manufacturing professionals, ensuring a pipeline of talent capable of driving efficiency and innovation in U.S. industries.