




What's Happening?
COFCO Engineering Equipment (Zhangjiakou) Co., Ltd., a prominent grain machinery manufacturer, is advancing modern grain processing solutions with its comprehensive portfolio of equipment and engineering services. The company, with roots dating back to
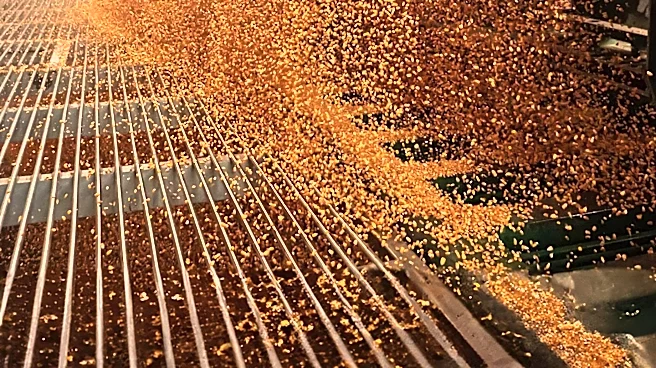
1959, specializes in grain cleaning, milling, conveying, storage, and related processing applications. Its product range includes advanced grain cleaning equipment, roller mills, plansifters, purifiers, and pneumatic conveying systems, designed to meet the increasing global demand for efficiency and product quality in agricultural and food-processing sectors. COFCO's MMR and MMRL Roller Mill series, for instance, features streamlined designs for easier maintenance and food-grade materials for contact with processed grain. The company emphasizes integrated engineering capabilities, providing solutions that cover the entire grain-processing workflow, from initial cleaning to final packaging. Its international presence extends to over 30 countries and regions, including markets in North and South America, where it has completed various grain-processing and flour-milling projects.
Why It's Important?
The advancements by COFCO Engineering Equipment are significant for the U.S. agricultural and food processing industries. As grain processors in North America seek higher efficiency and improved product quality, the availability of advanced machinery and integrated processing systems becomes crucial. COFCO's offerings, which include sophisticated grain cleaning and milling equipment, can help U.S. facilities enhance operational stability, protect downstream machinery, and produce consistent finished products. The company's focus on equipment integration means that U.S. grain processors can implement more automated and streamlined production lines, reducing bottlenecks and improving overall plant performance. This can lead to increased productivity and cost-effectiveness for American businesses involved in wheat flour mills, maize milling plants, and other grain processing operations, ultimately impacting the supply chain and consumer product quality.
What's Next?
COFCO Engineering Equipment is expected to continue its global expansion and technological development, further influencing the grain processing industry in the U.S. The company's ongoing investments in research and development, intelligent manufacturing, and digitalization suggest that future offerings will likely incorporate more advanced monitoring, automation, and data-driven solutions. This could lead to U.S. grain processors adopting more connected production environments, enabling better process optimization and predictive maintenance. As COFCO strengthens its manufacturing capabilities and international service model, U.S. customers can anticipate more comprehensive support, from project planning and customized solutions to installation, training, and after-sales service. This integrated approach could simplify project coordination for American companies looking to upgrade or establish new grain processing facilities.
Beyond the Headlines
Beyond the immediate operational benefits, COFCO's advancements highlight a broader trend towards sophisticated, integrated solutions in the global agricultural processing industry. For the U.S., this signifies a shift towards higher standards in food safety and efficiency, driven by technological innovation from international players. The emphasis on food-grade materials and quality management in COFCO's equipment reflects growing consumer and regulatory demands for safer food production practices, which will likely influence U.S. industry standards and compliance. Furthermore, the company's commitment to intelligent manufacturing and digital factories points to a future where grain processing facilities are highly automated and data-driven, potentially leading to new skill requirements for the U.S. workforce in this sector and fostering greater technological adoption across the agricultural supply chain.